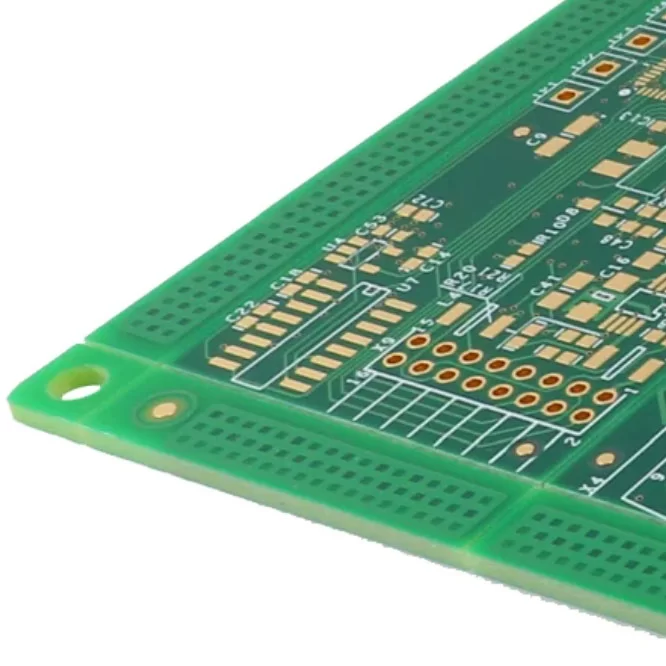
HAL Leaded (Hot Air Leveling - Leaded) and HASL RoHS (Lead-Free Hot Air Solder Leveling) are two common PCB surface finish processes used to protect copper pads and improve solderability. The primary difference lies in the solder alloy composition and environmental compliance.
HAL Leaded uses a traditional tin-lead (Sn-Pb) solder alloy, typically containing around 63% tin and 37% lead. It provides excellent solderability, lower processing temperatures, and reliable long-term performance. Due to its cost-effectiveness and ease of manufacturing, it is still widely used in industrial equipment and applications where RoHS compliance is not required.
HASL RoHS, also known as Lead-Free HASL, uses lead-free solder alloys such as tin-silver-copper (SAC). This finish complies with the RoHS (Restriction of Hazardous Substances) directive, making it suitable for products sold in Europe and many international markets. Although lead-free HASL requires higher processing temperatures and may have slightly different soldering characteristics, it offers excellent durability, environmental safety, and compatibility with modern electronic manufacturing standards.

Lead vs. Lead-Free Solder Property Comparison
Property | Lead Solder | Lead-Free Solder | Key Characteristic |
Melting point | Low and well-defined (≈183 °C) | Higher, broader range (≈217–227 °C) | Lead-free requires higher thermal input |
Thermal stress sensitivity | Low | Higher | Elevated temperatures increase stress risk |
Wetting behavior | Excellent wetting and flow | Reduced wetting | Lead-free needs optimized flux and profiles |
Joint appearance | Smooth and shiny | Dull or matte | Visual texture differs significantly |
Mechanical ductility | Soft and ductile | Harder and stiffer | Lead tolerates strain better |
Mechanical strength | Moderate | Higher | Lead-free joints resist deformation |
Fatigue resistance | Higher relative fatigue life | Often lower fatigue life under certain cyclic conditions | Cyclic stress favors lead solder |
Corrosion resistance | Adequate in controlled environments | Better in humid or corrosive conditions | Lead-free performs better in moisture |
Electrical conductivity | ~11.5 IACS | ~15.6 IACS | Lead-free slightly higher conductivity |
Thermal conductivity | ~50 W/m·K | ~73 W/m·K | Lead-free transfers heat more efficiently |
Electrical resistivity | Higher | Lower | Affects signal and power losses |
Surface tension | Lower (~481 mN/m) | Higher (~548 mN/m) | Higher tension reduces wetting |
Coefficient of thermal expansion (CTE) | Higher (~23.9 µm/m/°C) | Lower (~21.4 µm/m/°C) | Lead-free expands less with heat |
Density | Higher (~8.5 g/cm³) | Lower (~7.44 g/cm³) | Influences joint mass and vibration |
Shear strength | ~23 MPa | ~27 MPa | Lead-free joints are stronger |
Switching from Lead to Lead-Free Soldering
• Check equipment limits: Begin by confirming that all soldering equipment can operate reliably at higher temperatures. Lead-free alloys typically require tip and process temperatures in the range of about 350–400 °C, which can exceed the safe limits of older soldering irons and heaters. Reflow ovens and wave soldering systems must also provide stable, well-controlled temperatures to prevent excessive oxidation, pad damage, or component stress during prolonged exposure to heat.
• Select the right alloy: Choosing an appropriate lead-free alloy is needed to a smooth transition. For most general electronics work, SAC305 is widely used due to its balanced mechanical strength and process stability. For assemblies with heat-sensitive components or substrates, lower-temperature alternatives such as bismuth- or indium-based blends may be considered, provided they meet reliability and compatibility requirements for the application.
• Update thermal profiles: Lead-free soldering demands revised thermal profiles rather than simple temperature increases. The ramp rate, soak time, peak temperature, and cooling rate should all be optimized to ensure proper wetting while minimizing thermal stress. Using temperature profiling tools helps verify that the entire assembly stays within safe limits and reduces risks such as voids, warpage, or component damage.
• Avoid cross-contamination: Tools and equipment previously used with lead solder must be thoroughly cleaned before processing lead-free assemblies. Even small amounts of residual lead can mix with lead-free alloys, altering the joint composition and increasing the risk of brittle or unreliable connections. Dedicated tips, feeders, and storage areas are often used to maintain strict separation between alloy systems.
• Revise inspection standards: Visual inspection criteria should be updated to reflect the normal appearance of lead-free joints. Unlike lead solder, lead-free joints often have a matte or dull finish that does not indicate poor quality. For hidden or fine-pitch connections, such as BGAs, non-destructive methods like X-ray inspection become more important for detecting voids, bridges, or incomplete joints.
• Verify reliability: After process changes, reliability testing is important to confirm long-term performance. Thermal cycling and vibration tests are commonly used to evaluate how lead-free joints respond to mechanical and environmental stress. These tests help ensure that the new soldering process meets durability requirements for the intended operating conditions.
• Maintain compliance records: Finally, proper documentation supports regulatory compliance and quality control. This includes maintaining traceability of materials, clear labeling of lead-free products, and complete audit records. Accurate documentation helps demonstrate adherence to environmental regulations and simplifies customer or regulatory inspections in the future.
Advantages and Disadvantages of Lead and Lead-Free Solder
Advantages
Aspect | Lead | Lead-Free |
Ease of use | Very forgiving | Process-sensitive |
Melting behavior | Low and precise | Higher, more stable at heat |
Component stress | Lower | Higher |
Wetting | Excellent | Needs optimization |
Inspection | Shiny, clear | Matte appearance |
Tool life | Longer | Faster wear |
Compliance | Restricted | Globally accepted |
Disadvantages
Aspect | Lead | Lead-Free |
Health risk | Toxic | Safer |
Regulations | Restricted | Compliant |
Rework | Faster | Slower |
Tip wear | Lower | Higher |
Tin whiskers | Suppressed | Higher risk |
Cost | Lower | Higher |
PCB damage risk | Lower | Higher if mis-profiled |
Uses of Lead vs Lead-Free Solder
Lead Solder
• Legacy electronics repair, where older boards were designed for tin–lead solder behavior
• PCBs originally specified for lead solder, which may be damaged by higher lead-free temperatures
• Laboratories, training, and prototyping, due to easier handling and consistent joint formation
• Aerospace and defense applications, where regulatory exemptions allow lead solder for proven reliability
• Low-temperature or precision rework, especially for heat-sensitive components and fine-pitch joints
Lead-Free Solder
• Modern consumer electronics, such as smartphones, laptops, and home appliances
• Automotive electronics, where compliance and durability under wide temperature ranges are required
• Medical devices, to reduce toxic material exposure and meet safety standards
• Industrial and communication systems, supporting long-term compliance and reliability
• RoHS-regulated markets, where lead-free solder is mandatory for legal market access
Lead vs Lead-Free Common Soldering Defects
Defect | Main Cause | Impact | Lead Behavior | Lead-Free Behavior |
Cold joint | Low heat, movement | Weak connection | Less common | More common |
Poor wetting | Oxidation, weak flux | High resistance | Usually wets well | Needs tighter control |
Bridging | Excess solder, fine pitch | Shorts | Lower risk | Higher risk |
Voids | Flux outgassing | Lower strength | Less frequent | More frequent |
Dull appearance | Cooling/oxidation | Inspection issues | Shiny | Matte but normal |
Pad lifting | Excess heat | Permanent damage | Lower risk | Higher risk |
Tin whiskers | High-tin stress | Latent shorts | Suppressed | Requires mitigation |
Conclusion
Lead and lead-free solders each serve distinct purposes shaped by performance needs, process limits, and regulatory demands. While lead-free solder dominates modern manufacturing, lead solder remains relevant in specific controlled or exempt applications. A clear understanding of alloy behavior, processing impacts, and long-term reliability enables informed solder selection that balances compliance, quality, and operational success.
Frequently Asked Questions [FAQ]
Is lead-free solder compatible with boards originally designed for lead solder?
Lead-free solder can be used on older boards, but higher process temperatures increase the risk of pad lifting and component damage. Careful profiling and low-temperature lead-free alloys may be required to reduce stress.
Why does lead-free solder look dull even when the joint is good?
Lead-free alloys naturally solidify with a matte or grainy surface due to their microstructure. Unlike lead solder, a dull appearance does not indicate a poor or cold joint if wetting and fillet shape are correct.
Does lead-free solder reduce product reliability over time?
Not inherently. When processes are optimized, lead-free solder can achieve long-term reliability comparable to lead solder. Issues usually arise from improper thermal profiles, alloy selection, or insufficient inspection methods.
Can lead and lead-free solders be mixed during rework?
Mixing is strongly discouraged. Even small amounts of lead contamination can change alloy behavior, lower melting predictability, and create brittle joints that reduce mechanical and thermal reliability.
Which solder type causes more wear on soldering tips and equipment?
Lead-free solder causes faster tip erosion and oxidation due to higher operating temperatures and increased tin activity. This often results in shorter tip life and higher maintenance costs compared to lead solder.